Part 5: From survey data to economic decisions
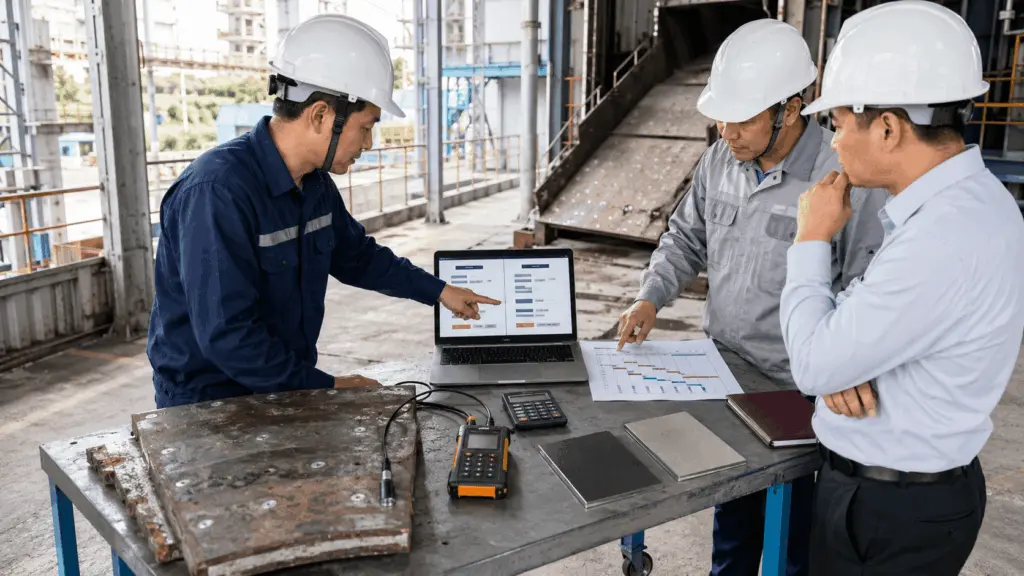
When a location already has data on wear rate, remaining service life, and maintenance cycles, the question is no longer limited to which material lasts longer. The plant needs to know which solution is better aligned with the operating cycle and results in a more reasonable cost of use.
The distinction that needs to be made from the outset is between material purchase cost and costs incurred during use. Price per kilogram reflects only the amount paid to purchase the material. The actual cost of a solution is also related to the number of replacements, equipment downtime, labor, and the effect on operations.
Therefore, wear measurements only truly support economic decision-making when they are linked to the plant’s maintenance cycles and operating data.
1. Purchase price does not reflect the full cost of use
Price per kilogram indicates the purchase cost, but does not show how many times the material needs to be replaced each year, how long the equipment needs to be stopped for each replacement, how many labor hours are required, or whether the location has previously caused unplanned shutdowns.
Two solutions with different purchase prices therefore cannot be compared solely on the basis of unit price.
A material with a higher purchase price but capable of operating through multiple maintenance cycles may create a completely different cost profile from a lower-priced material that requires frequent replacement.
The point of comparison is the cost of each solution over the same period of time or the same operating cycle, rather than placing the purchase price of one solution next to the service life of the other.
2. Before calculating cost, check whether the service life extends beyond the maintenance cycle
An increase in service life creates a clear operational difference only when it allows the location to pass a maintenance milestone that is meaningful to the plant.
For example, a plant may have a fixed maintenance shutdown schedule, but the new material may still require replacement before the next scheduled shutdown. In that case, the additional service life may not necessarily reduce the actual number of interventions.
Therefore, before preparing the cost table, it is necessary to determine whether the new solution enables the location to operate through one additional maintenance cycle.
This is the step that connects technical data with the operating schedule: the material not only needs to last longer, but long enough to change how the plant organizes maintenance.
3. Four input data points are required before calculating cost
An economic calculation is only meaningful when the input data are clearly defined.
The four required figures are the production output value per hour of the line, the number of downtime hours per intervention, the number of interventions per year, and the material and labor cost per intervention.
Most of these data belong to the plant itself. The material supplier should not estimate them independently if the figures have not been confirmed by the plant.
A spreadsheet may be mathematically correct yet still produce an unreliable result if the input figures do not reflect the actual operating conditions.
4. From wear rate to the number of interventions
The wear rate in mm/month needs to be converted into the remaining time before the location reaches the replacement threshold.
The conversion consists of three steps:
The replacement threshold is the minimum remaining thickness that the plant accepts for the location to continue operating. This value is determined by the plant because it is directly related to operation and safety.
The supplier may perform analysis and provide technical recommendations but does not establish the threshold on behalf of the plant.
The method for measuring wear rate, establishing the baseline, and using the replacement threshold is presented in Part 4: Measuring wear rate and establishing a baseline.
5. Convert the number of interventions into annual cost
Once the number of interventions has been determined, the cost items can be converted to the same time period for comparison.
Basic formula:
Annual cost = Number of interventions × (Downtime × Downtime value per hour + Labor + Material)
The purpose of this calculation is to place the solutions on the same basis for comparison. It is not a complete cost model for every plant.
The important point is to avoid presenting one solution in terms of price/kg while the other is presented in terms of service life or number of replacements. Two solutions can only be compared when the same units and the same time period are used.
6. Place the solutions in the same comparison table
The current solution and the proposed solution need to be placed side by side using the same calculation method.
The table does not need an additional “percentage savings” column calculated independently by the supplier.
Once the input data are clear, the plant can directly see the difference between the two solutions. This presentation keeps the table in its proper role as a comparison support tool, rather than turning the result into a sales claim.
7. The data source needs to be recorded together with each indicator
An economic comparison table usually combines three different types of information: field measurements, data provided by the plant, and results calculated from input data.
Instead of using abbreviated labels, the nature of each group should be stated clearly:
Recording the source allows the reader to know which values were measured, which belong to the plant’s operating data, and which are calculation results.
This is particularly important when multiple data sources are used together to produce an economic result.
8. Not every impact should immediately be converted into a monetary value
Some factors may significantly affect the decision but do not yet have a sufficient basis to be converted into a specific monetary value.
If there is not yet a sufficiently clear basis, an estimated figure should not be placed alongside measurements and confirmed data.
An unsupported estimate can reduce the reliability of the entire comparison table.
9. Three items to check before using the cost table
Before sending the table to the procurement department or plant management, three items need to be checked:
- the source of each indicator has been clearly identified
- figures belonging to the plant’s operating data have actually been provided or confirmed by the plant
- whether the table is independently drawing a “percentage savings” conclusion instead of presenting the two solutions on the same calculation basis
Among these, the sources of data such as downtime value per hour, maintenance cycle, and replacement threshold are particularly important. If these figures do not accurately reflect the plant’s conditions, all subsequent calculations will be affected.
10. The same table serves different purposes for different departments
A single comparison table can be shared, but each department will focus on a different group of data.
For engineering, the focus is on wear rate, service life, and the number of operating cycles that can be completed.
For procurement, the focus shifts to material cost, cost per cycle, and annual cost.
For plant management, the number of interventions, equipment downtime, and the effect on operations are often more meaningful than an individual material unit price.
Therefore, terms such as “cheaper” or “more cost-effective” are only meaningful when the solutions have been placed on the same calculation basis.
11. Responsibilities of the departments
The cost table is only reliable when responsibility for providing data, performing calculations, and selecting the solution is clearly defined.
The principle that needs to be maintained is that the material supplier does not independently fill in figures that belong to the plant.
When an input value has not yet been determined, it should be left blank or clearly marked as requiring additional information, rather than creating an estimated value solely to complete the calculation.
12. Notes when applying this knowledge
First, this is a conversion method for comparing solutions, not a complete cost model for every plant. A broader model may also involve depreciation, inventory, and production planning.
Second, factors such as the risk of unplanned shutdown, capacity limitations, or compliance risks should not be independently converted into monetary values when there are insufficient supporting data.
Third, the calculation depends directly on the plant’s data. When the downtime value per hour, maintenance cycle, or replacement threshold is missing, an economic result with the same level of reliability as one based on complete input data cannot yet be produced.
Moving from wear measurements to economic decision-making is the process of bringing technical data onto the same operating basis. A solution can only be meaningfully compared when service life, number of interventions, equipment downtime, and cost are all calculated under the same conditions and using data with clearly identified sources.